Reviewed
Flocculation guidanceCoagulant Before Polymer: Why Sequence Controls Floc Strength
Review coagulant and polymer sequence using the actual feed chemistry and mixing route before attributing weak floc to the PAM grade.
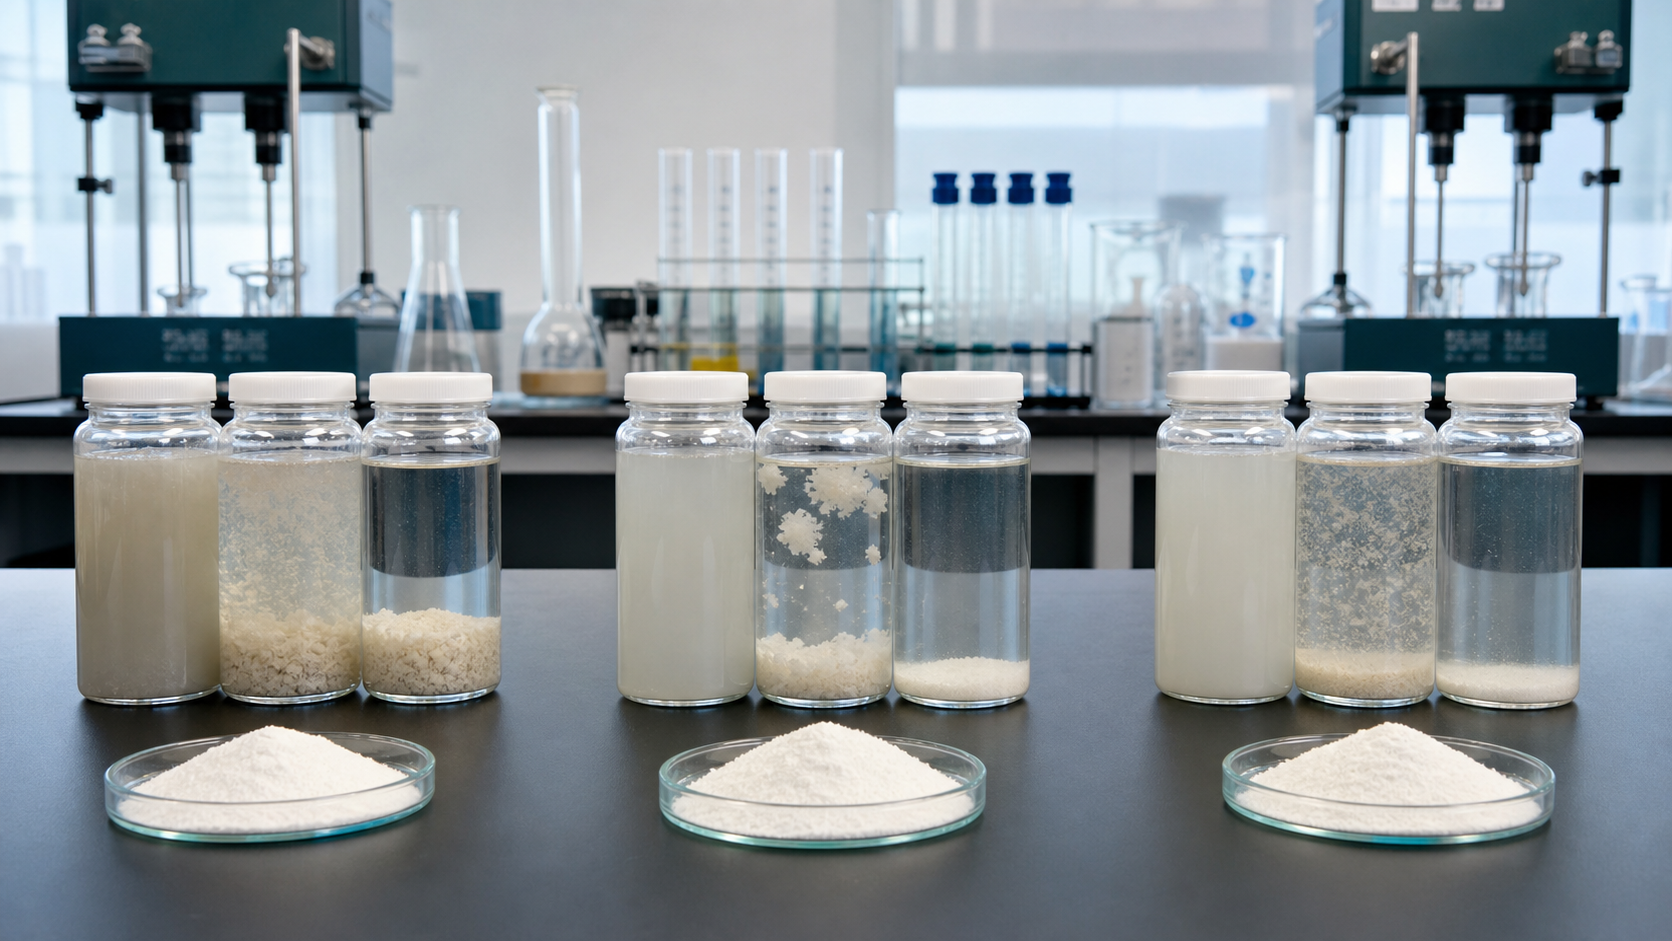
Process image for polymer treatment planning.
The operating situation is a plant combining inorganic coagulant with polyacrylamide for difficult wastewater, yet adding chemicals in the wrong order wastes charge neutralization and weakens bridging. A useful answer must connect chemistry with hydraulics, equipment, solids handling, and cost. Changing a polymer setpoint without checking those conditions can improve one reading while making the overall process less stable.
Establish the Baseline
Record pH shift, coagulant dose, flash mix, polymer contact time, floc size, and clarified water. Use the same sampling points and time basis before and during the trial. The baseline should cover normal operation and at least one representative high-load period; otherwise the selected dose may work only on the easiest water.
Translate every chemical setting into a common dose basis. State whether the number refers to neat product, active polymer, or prepared solution, and reconcile calculated demand with bag or tote drawdown. For the coagulant before polymer sequence floc strength calculation, that unit discipline prevents a pump-speed comparison from being mistaken for a product-performance comparison.
Diagnose the Limiting Step
Start where the symptom first appears. Inspect feed variability, pH, conductivity, solids concentration, upstream chemicals, mixing energy, residence time, sludge inventory, and withdrawal capacity. The fact that adding chemicals in the wrong order wastes charge neutralization and weakens bridging may point to chemistry, but it can also expose a hydraulic or mechanical constraint that additional polymer will not correct.
Take samples before polymer addition, after rapid dispersion, after low-shear flocculation, and at the separation outlet. Comparing those locations shows whether floc never forms, forms and then breaks, settles but is carried over, or creates sludge that the plant cannot remove quickly enough.
Screen Products on Representative Water
Run a blank and compare a small family of candidates over low, middle, and high doses. Keep preparation concentration, solution age, mixing sequence, settling time, and evaluation method constant. The best result is not automatically the largest visible floc; it is the condition that produces repeatable separation and manageable solids across a usable dose window.
The proposed product is coagulant followed by matched PAM. Treat that description as a trial hypothesis rather than a guaranteed grade. Mineral fines often lead to anionic screening, organic or biological sludge often requires cationic candidates, and high salinity or mixed industrial water can change both assumptions. Site water decides the shortlist.
Scale the Bench Result to the Plant
Convert the selected bench dose to actual flow, dry-solids load, or treated volume. Confirm make-down capacity, aging time, pump turndown, injection location, and available contact time at minimum and maximum flow. If full-scale shear differs from the jar test, adjust the trial method before rejecting the chemistry.
Change one controlled variable at a time and allow the process to reach steady state. Collect paired inlet and outlet results, operator observations, sludge measurements, and chemical consumption. A short clear-water interval is not enough evidence when the intended result is stronger floc and lower total chemical cost.
Judge Performance and Cost Together
Define acceptance criteria before supplier representatives arrive. Water quality may include turbidity, TSS, filtrate solids, filter differential pressure, or reuse stability. Solids criteria may include capture, cake solids, underflow density, sludge volume, or rake torque. Cost should include active dose, labour, packaging, downtime, hauling, and downstream cleaning rather than price per kilogram alone.
Coagulant and polymer are partners, but they are not interchangeable. If a higher-priced grade reduces active dose, improves solids capture, or prevents a disposal penalty, it may be the lower-cost operating choice. If performance depends on a narrow dose that operators cannot hold, the apparent laboratory winner may be unsuitable.
Procurement and Supply Questions
Request a technical data sheet, safety information, batch identification, preparation guidance, packaging options, lead time, storage limits, and evidence of repeat supply. Ask the supplier to state what would trigger retesting. A trial report should preserve raw data, unsuccessful doses, feed conditions, and the agreed acceptance calculation.
Manufacturer context is available from Gongyi Xinqi Polymer Co., Ltd.. Related product and application references include anionic polyacrylamide and polyacrylamide manufacturers. These sources help frame questions, but the purchase decision should remain tied to the site's sample and verified full-scale result.
Decision Summary
For coagulant before polymer sequence floc strength, move from baseline to diagnosis, controlled screening, scale-up, and total-cost review. The desired outcome is stronger floc and lower total chemical cost. Documenting that chain gives operations a stable control range and gives procurement evidence that can be compared across suppliers and future batches.